Share on X
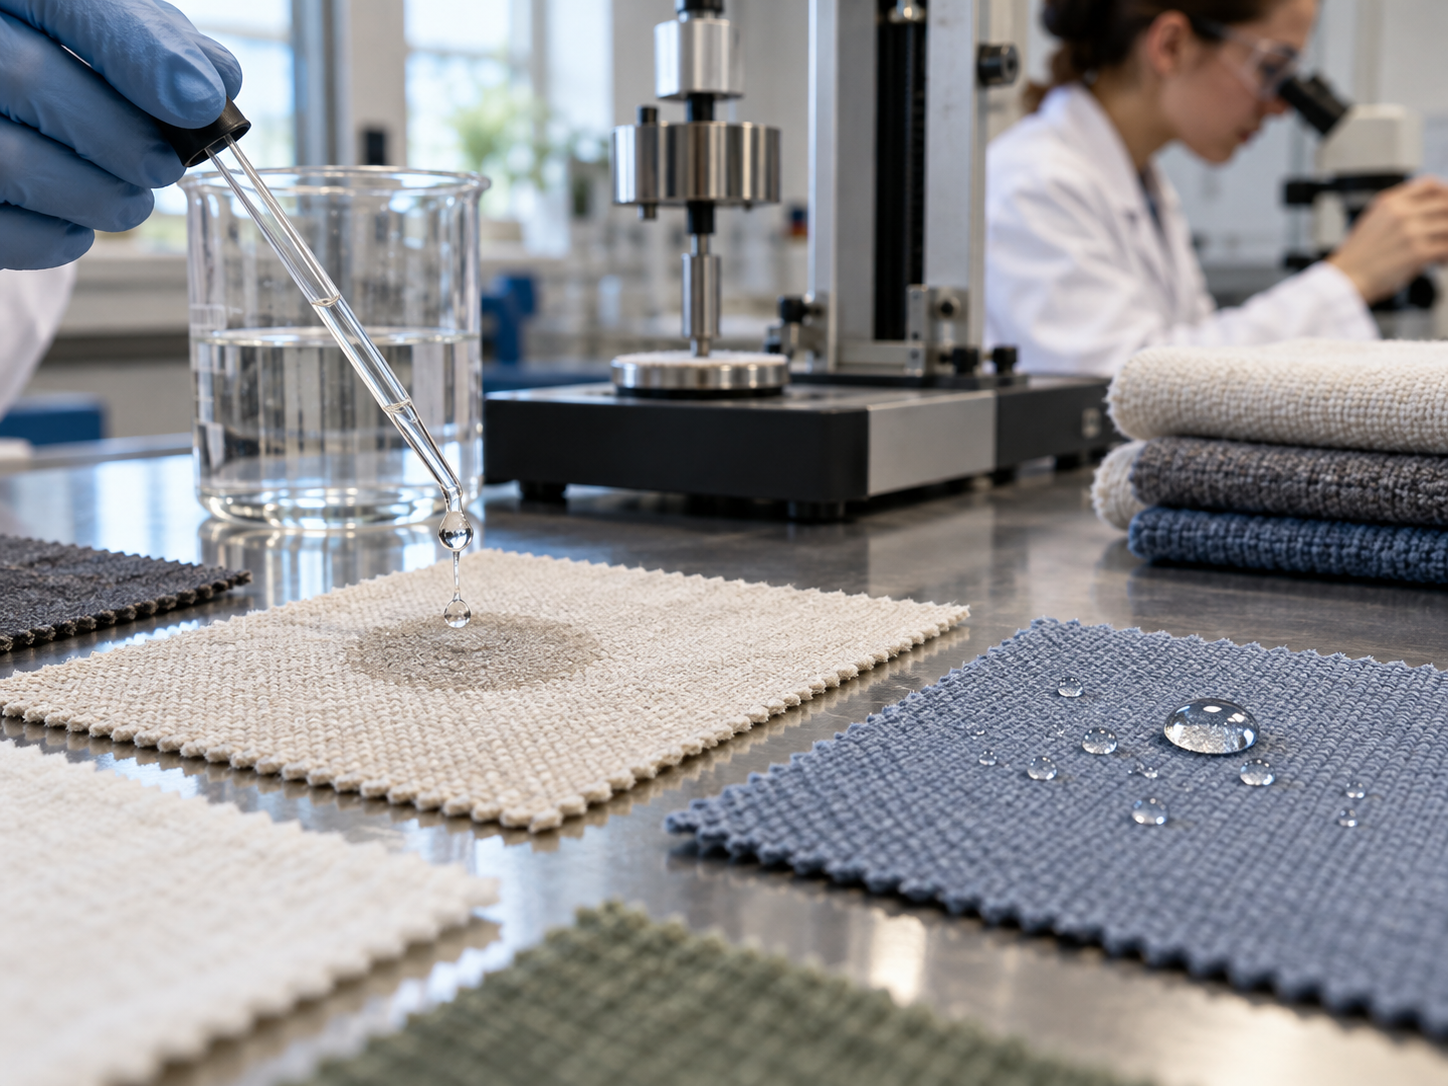
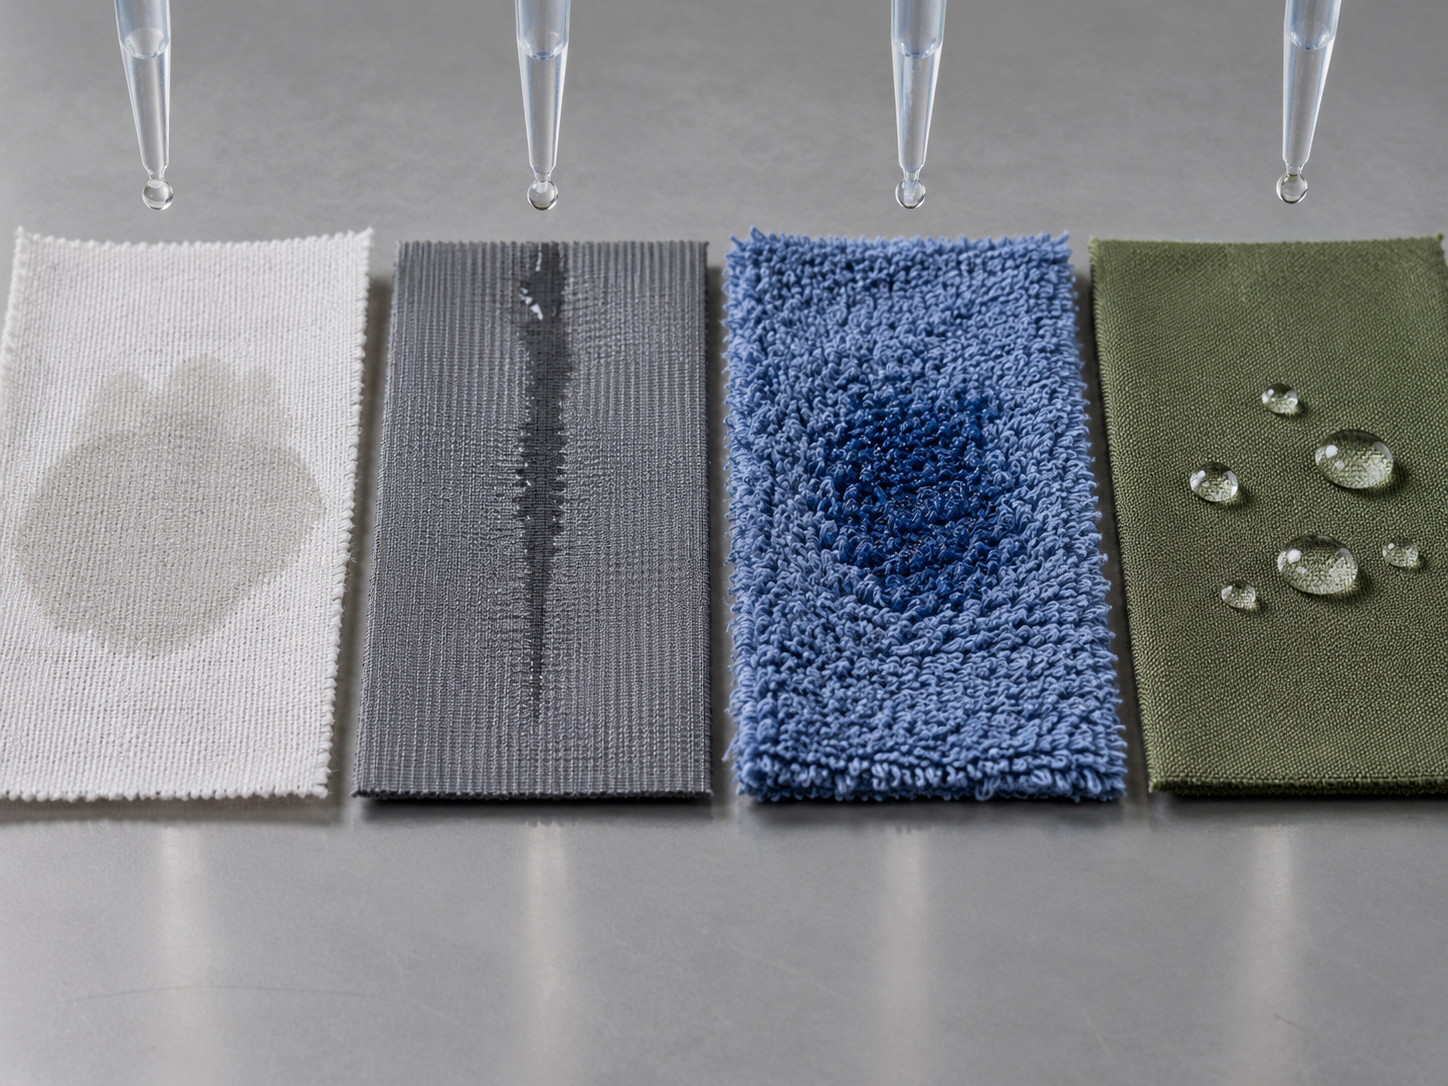
Absorbency in textiles is the ability of a fiber, yarn, fabric, or finished product to take up and retain liquid. Although the term is often used casually to describe anything that becomes wet, textile absorbency is a more complex performance characteristic governed by surface chemistry, internal fiber structure, yarn geometry, fabric construction, finishing treatments, and the physical pathways through which liquid can move.
Absorbency matters wherever a textile must remove, distribute, store, or manage liquid. Towels must rapidly collect water from skin; wipes and medical nonwovens may need both rapid uptake and adequate liquid capacity; apparel often requires controlled moisture transport rather than maximum retention; and textile processing operations depend on predictable wetting so that dyes, bleaches, finishes, and other aqueous treatments penetrate evenly. A fabric that absorbs a large quantity of water slowly may therefore perform very differently from one that wets and transports liquid quickly.
Understanding absorbency requires distinguishing several related concepts: wetting, absorption, adsorption, capillary action, wicking, moisture regain, drying, repellency, and resistance to water penetration. Modern textile testing consequently uses different methods for different end uses rather than treating absorbency as a single universal property.
What Absorbency Means in Textile Science
In textile practice, absorbency describes the uptake of liquid by a textile material. The liquid may enter the fiber itself, occupy spaces between fibers and yarns, spread through capillary channels, or be retained through a combination of these mechanisms. The measured result therefore depends on both material chemistry and textile structure.
Absorption generally refers to penetration of a substance into the bulk of another material. Adsorption, by contrast, concerns molecules accumulating at a surface. Both can occur in fibrous materials, but everyday textile discussions commonly use absorbency as the broader practical term for liquid uptake.
Several related properties should not be treated as synonyms. Wetting describes how readily a liquid establishes contact with a surface. Wicking is liquid transport through capillary spaces in fibers, yarns, or fabric structures. Moisture regain normally concerns equilibrium moisture absorbed from the atmosphere relative to dry fiber mass, rather than the rapid uptake of bulk liquid water. Water repellency describes resistance to wetting, while water resistance concerns resistance to liquid penetration under specified conditions.
Consequently, asking whether a textile is absorbent is incomplete unless the required performance is defined. Important questions include how rapidly it wets, how much liquid it can hold, whether it spreads the liquid, whether it releases liquid under pressure, and how quickly it dries afterward.
How Fiber Chemistry Influences Liquid Uptake
Fiber chemistry strongly affects how readily water interacts with a textile. Fibers containing polar or hydrophilic chemical groups generally have greater affinity for water than strongly hydrophobic polymers. Cellulosic fibers such as cotton, flax, and regenerated cellulose contain numerous hydroxyl groups capable of interacting with water. Their internal morphology and accessible regions allow moisture to enter the fiber as well as the surrounding capillary structure.
Synthetic fibers such as conventional polyester are comparatively hydrophobic. They may absorb relatively little water into the polymer itself, yet fabrics made from them can still transport substantial liquid through engineered capillary channels. This distinction is central to modern moisture-management textiles: low intrinsic fiber absorption does not necessarily mean poor liquid movement.
Natural fibers also carry surface materials that can alter wetting. Raw cotton, for example, contains non-cellulosic substances including waxes that reduce immediate water wettability. Textile preparation processes such as scouring remove much of this material and improve access of aqueous processing liquors to the cellulose.
Fiber cross-section, diameter, surface roughness, internal pores, crystallinity, and chemical modification can further influence liquid behavior. For this reason, absorbency cannot reliably be predicted from generic labels such as natural or synthetic alone. The finished textile must be evaluated as a complete system.
Wetting, Capillary Action and Wicking
Before water can be absorbed or transported efficiently, it must wet the textile surface. Wetting depends partly on the relationship between the surface energy of the solid and the surface tension of the liquid. Oils, waxes, silicone treatments, fluorinated finishes, contaminants, and other low-surface-energy substances can hinder wetting even when the underlying fiber would otherwise interact strongly with water.
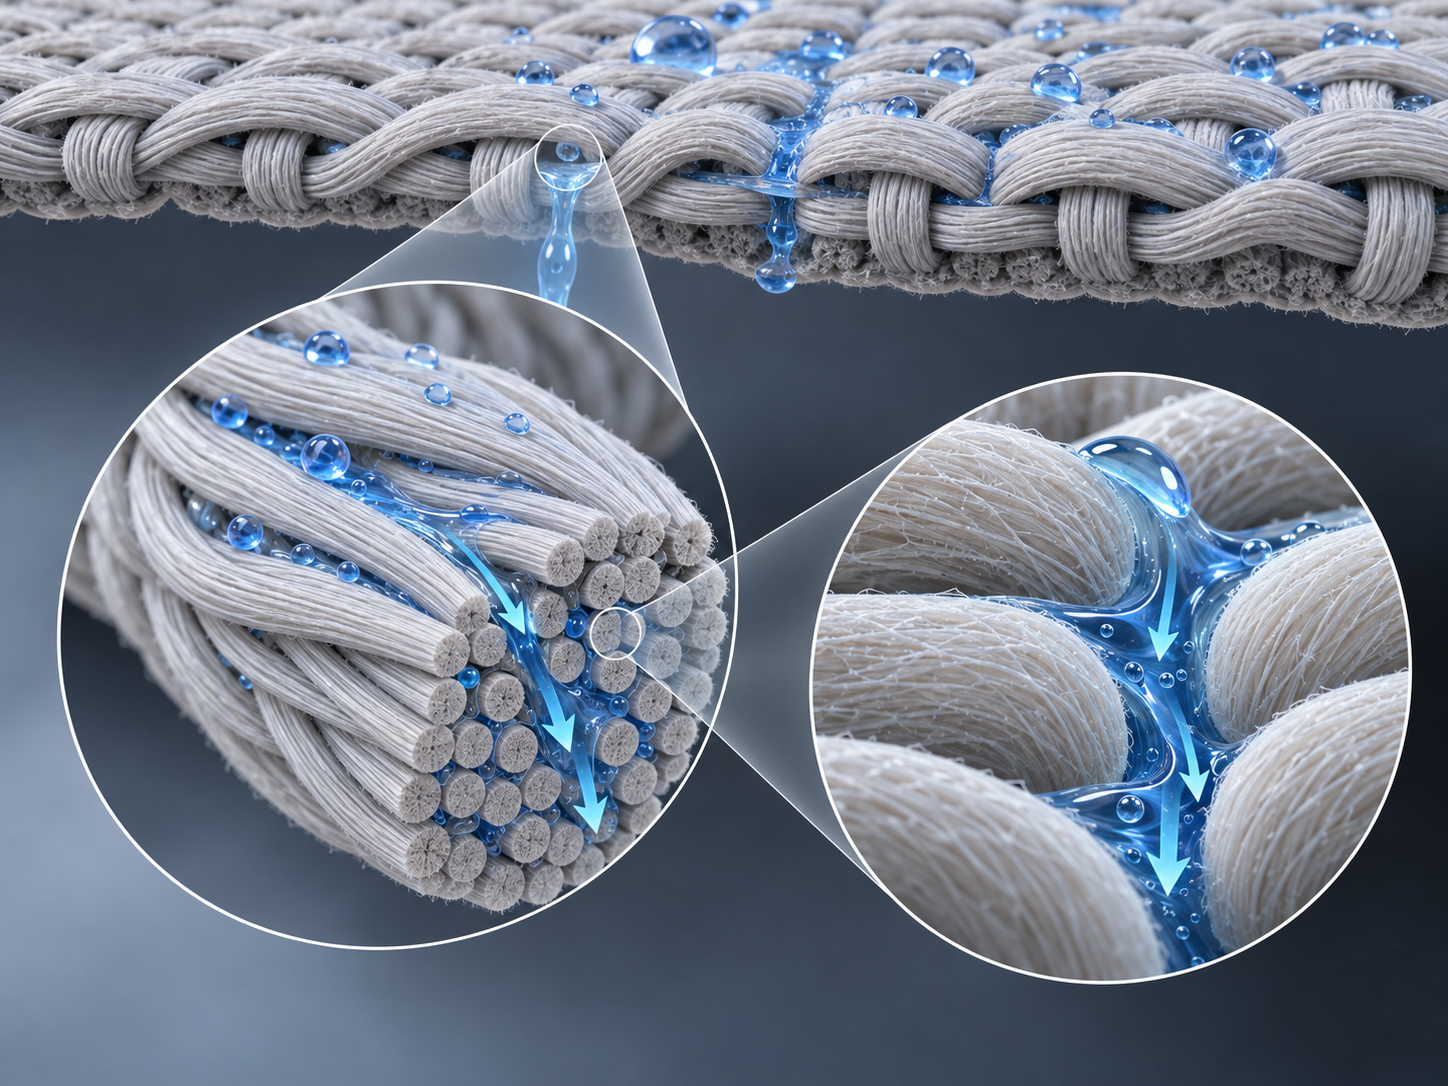
Once wetting occurs, liquid may move through narrow spaces between fibers and within yarn structures by capillary action. These channels can draw liquid away from the original point of contact. The rate and direction of movement depend on factors including pore size, surface chemistry, yarn twist, filament arrangement, fabric density, and gravity.
Wicking is therefore primarily a transport phenomenon. A fabric can wick effectively without storing large quantities of water inside its fibers. Performance polyester sports fabrics illustrate this principle: engineered yarns and structures may move perspiration across a larger surface area so that evaporation becomes easier, even though the polymer itself has comparatively low moisture absorption.
Conversely, a material with high liquid-holding capacity may feel saturated if it retains water rather than distributing or releasing it. Textile engineers therefore separate initial wetting, transport rate, spreading area, absorptive capacity, retention, and drying when evaluating moisture-management systems.
Yarn and Fabric Structure Can Be as Important as Fiber Type
Absorbency is created not only by fiber chemistry but also by the architecture of the textile. Yarn construction determines the size, continuity, and accessibility of capillary pathways. Twist, filament count, staple arrangement, bulk, texturing, and blending can all influence liquid transport.
Fabric construction introduces another scale of porosity. Loosely structured fabrics may admit liquid rapidly but may not necessarily retain it. Dense constructions can slow penetration. Knitted loops, woven interlacements, nonwoven fiber networks, and pile structures each create characteristic pathways for liquid.
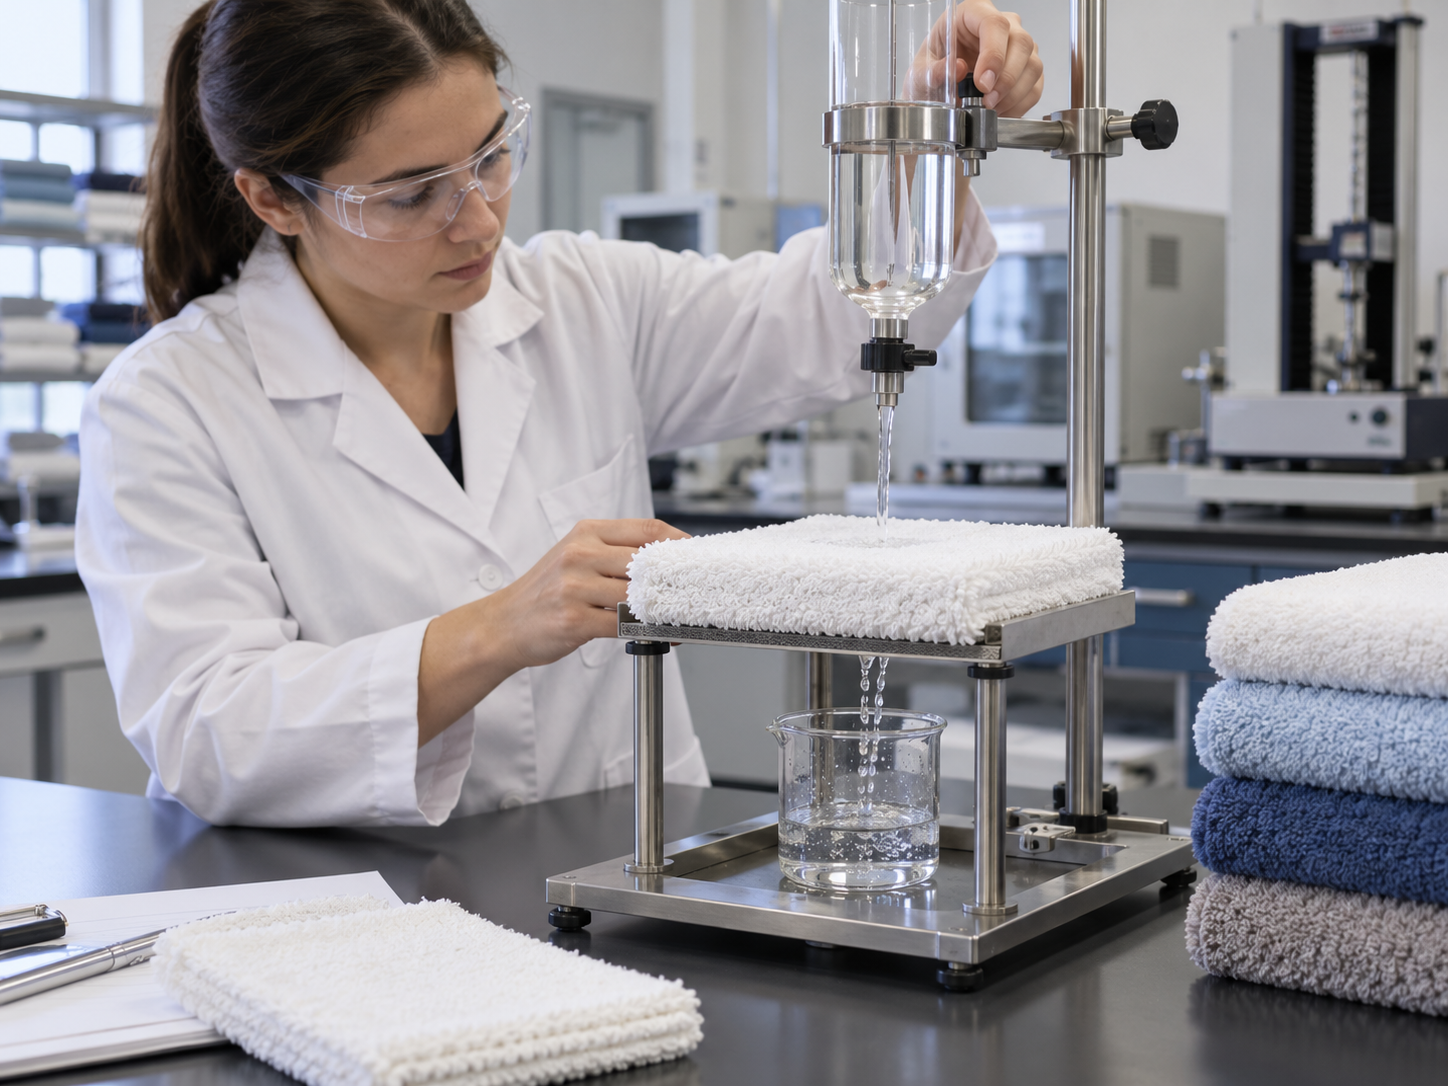
Terry towels demonstrate how construction can amplify practical absorbency. Their pile loops create a large accessible surface area and substantial void volume capable of receiving and retaining water. This is why ASTM maintains a test specifically for the surface water absorption of terry fabrics rather than assuming that a generic fabric absorbency test fully predicts towel performance.
Nonwoven absorbent products present another distinct structure. Fiber webs can be engineered for rapid strike-through, liquid distribution, storage, or combinations of these functions. ISO 9073-6 addresses nonwoven absorption through separate measures including absorbency time, absorptive capacity, and wicking rate, illustrating that even within one textile class, absorbency is multidimensional.
Textile Processing and Finishing Effects
Wet processing can dramatically change absorbency. Preparation stages such as desizing, scouring, and appropriate bleaching remove substances that interfere with wetting and help fabrics accept subsequent aqueous treatments more uniformly. Insufficient preparation can produce uneven dyeing or finishing because parts of the textile resist penetration.
Finishes may either increase or decrease liquid affinity. Hydrophilic finishes can improve wetting and moisture transport on otherwise poorly wettable textiles. Conversely, durable water-repellent treatments are deliberately designed to resist surface wetting. Softener chemistry, lubricants, resins, coatings, printing binders, and other treatments may also alter absorbency intentionally or unintentionally.
Laundering can change performance again. Residual detergents, fabric conditioners, oils, soil, finish degradation, and repeated mechanical action can modify the way a textile wets and transports water. A product therefore may not retain its original absorbency throughout its service life.
For quality control, absorbency should be evaluated at the manufacturing stage that corresponds to the intended specification. A greige fabric, prepared fabric, finished fabric, laundered product, and worn product may give very different results even when their fiber composition and basic construction are unchanged.
How Textile Absorbency Is Tested
There is no single test that describes every aspect of textile absorbency. A suitable method must reproduce the performance question relevant to the product.
AATCC TM79, Absorbency of Textiles, is intended for determining water absorbency in yarns, fabrics, and garments and can be applied across woven, knitted, and nonwoven constructions. It provides a standardized framework for assessing whether a textile accepts water under defined conditions.
ASTM D4772 addresses a different problem: the ability of terry fabric to rapidly absorb and retain liquid water from a surface. ASTM identifies uses such as towels, washcloths, and similar terry products and notes that the method is specifically designed for this construction rather than non-terry fabrics.
ISO 9073-6:2025 covers absorption behavior of nonwovens and separates performance into liquid absorbency time, liquid absorptive capacity, and liquid wicking rate. This distinction is important because rapid uptake, total capacity, and capillary movement are not equivalent properties.
For fabrics intended to manage perspiration or other moving moisture, AATCC provides additional methods. TM195 evaluates liquid moisture-management properties using characteristics associated with resistance, repellency, absorption, fabric geometry, and wicking. TM217-2025 measures vertical and horizontal liquid spreading by image analysis. The choice of method should therefore follow the intended end use rather than convenience alone.
Absorbency, Moisture Regain and Moisture Content
Absorbency is often confused with moisture regain and moisture content because all three involve water in textiles. They describe different measurement situations.
Moisture regain expresses the mass of moisture in a conditioned textile relative to its oven-dry mass. It is especially important in fiber trading, processing, dimensional behavior, electrostatic performance, and standard textile conditioning. Moisture content expresses moisture relative to the total mass of the moist material. Both typically concern equilibrium or near-equilibrium moisture rather than rapid liquid uptake.
Liquid absorbency, by contrast, may involve direct contact with liquid water and may be evaluated through wetting time, uptake capacity, surface water removal, or liquid transport. A towel may be assessed for how efficiently it collects water from skin, whereas a fiber sample may be conditioned to determine atmospheric moisture regain.
These differences matter commercially. A high moisture-regain fiber does not automatically produce the best towel, wipe, or sports fabric. Product performance emerges from fiber properties combined with yarn geometry, fabric structure, finishing, laundering history, and the conditions of use.
Applications Across Textile Products
Absorbency requirements vary sharply by application. Bath and kitchen textiles require rapid surface water removal combined with useful holding capacity. Cleaning wipes may require fast uptake, strong retention, controlled release, or compatibility with cleaning fluids. Medical and hygiene textiles may require carefully engineered liquid acquisition and distribution within multilayer structures.
In apparel, maximum absorption is not always desirable. Everyday cellulosic garments can provide comfortable moisture interaction, but performance clothing often aims to move sweat away from the skin and expose it to a larger evaporative area. In such products, wicking rate and drying behavior may matter more than absolute water-holding capacity.
Dyeing, printing, bleaching, and chemical finishing also depend on controlled wetting. A fabric that does not wet uniformly can develop processing irregularities because treatment liquor reaches different regions at different rates. Absorbency testing can therefore function as a preparation-quality check before expensive downstream processes.
Technical textiles add further requirements. Filtration media, industrial wipes, geotextiles, absorbent nonwovens, and composite reinforcement systems may interact with water or process fluids in very different ways. Specifications must consequently identify the relevant liquid, test conditions, rate, capacity, retention, and structural requirements rather than relying on the general word absorbent.
Performance Trade-Offs and Common Misinterpretations
High absorbency is not universally beneficial. A textile that holds large amounts of water may become heavy, dry slowly, change dimensions, or feel clammy. In activewear, retaining perspiration can be less desirable than transporting it away from the skin. In protective outdoor clothing, water uptake may directly conflict with the requirement for repellency.
Another common mistake is judging absorbency solely by fiber content. Cotton-rich products may be strongly absorbent after suitable preparation, but construction and finishing can either reinforce or suppress that behavior. Polyester is intrinsically less hydrophilic, yet engineered polyester fabrics can display excellent capillary transport. Blended textiles create further combinations of uptake, transport, strength, durability, and drying behavior.
Laboratory results must also be interpreted carefully. A drop test, vertical-wicking test, absorptive-capacity test, and terry water-flow test measure different responses and should not be compared as if they represented the same property. Temperature, textile conditioning, water quality, specimen orientation, previous laundering, and sampling can also affect results.
Good specifications therefore define the performance mechanism rather than simply stating that a fabric should be absorbent. The correct question is whether the textile wets, transports, stores, releases, or evaporates liquid at a rate appropriate to its intended use.
Sustainability and Product-Life Considerations
Absorbency has sustainability implications because moisture behavior affects processing, product care, drying energy, durability, and functional lifetime. Textile preparation intended to improve wettability consumes water, energy, and chemicals, so mills increasingly seek efficient processing conditions and accurate process control rather than unnecessarily intensive treatment.
During use, highly water-retentive products may require more energy or time to dry. Conversely, low-retention moisture-management fabrics can dry more quickly but may rely on synthetic polymers or chemical finishes whose environmental impacts must be evaluated across the complete product system. No single absorbency profile is inherently sustainable.
Durability is also important. If an absorbent finish loses effectiveness after a few laundering cycles, the functional life of the product may be shortened. A structure that achieves performance through durable fiber and yarn geometry may retain functionality differently from one dependent primarily on a surface treatment.
For product development, the strongest approach is lifecycle-oriented: specify the required liquid-management function, minimize unnecessary chemistry and processing, test durability after realistic care cycles, and evaluate water and energy requirements during manufacture and use. Absorbency should therefore be treated as part of an integrated performance design rather than as an isolated laboratory number.
Standards Organizations and Current Industry Practice
Several standards organizations provide the framework through which textile absorbency and moisture management are evaluated. The American Association of Textile Chemists and Colorists maintains TM79 for textile absorbency together with a broader family of moisture-management methods covering wicking, drying, and liquid transport. Its current testing program treats absorbency and moisture management as related but distinct areas of textile performance.
ASTM International publishes application-specific methods including ASTM D4772 for surface water absorption of terry fabrics. Its scope illustrates a central principle of textile testing: a method designed for one construction and use should not automatically be generalized to other fabrics.
The International Organization for Standardization publishes ISO 9073-6 for nonwoven absorption testing. The 2025 edition identifies absorbency time, absorptive capacity, and wicking rate as separate aspects of liquid interaction.
Current industry practice increasingly combines these standardized measurements with application-specific product testing, image analysis, instrumented moisture mapping, laundering durability studies, and controlled wear or use trials. The trend is away from describing fabrics simply as absorbent and toward quantifying how moisture enters, moves through, remains in, and leaves the textile system.
Why Absorbency Remains a Core Textile Performance Property
Absorbency is best understood as a textile-system property rather than a simple characteristic of a fiber. Fiber chemistry determines how strongly a material interacts with water, but yarn arrangement, pore structure, fabric construction, surface contamination, preparation, finishing, and laundering can change the observed behavior substantially. Practical performance therefore depends on both the material and the pathways available for liquid movement.
The most useful distinction is between the different stages of moisture interaction. Wetting determines whether liquid can enter the structure; capillary action and wicking determine how it moves; absorptive capacity describes how much can be retained; and drying governs how rapidly that moisture leaves. Moisture regain and moisture content describe related but different equilibrium phenomena. Recognizing these distinctions prevents misleading comparisons between towels, apparel, nonwovens, wipes, and technical textiles.
As textile products become more application-specific, absorbency testing is becoming correspondingly precise. Standards from AATCC, ASTM International, and ISO already separate general absorbency, terry surface-water removal, nonwoven capacity, wicking, drying, and multidirectional moisture transport. Future textile development will increasingly combine durable fiber engineering, fabric architecture, lower-impact processing, and quantitative moisture mapping. For manufacturers and designers, the central goal is no longer maximum absorbency, but the right balance of wetting, transport, storage, release, and drying for a clearly defined end use.