Share on X
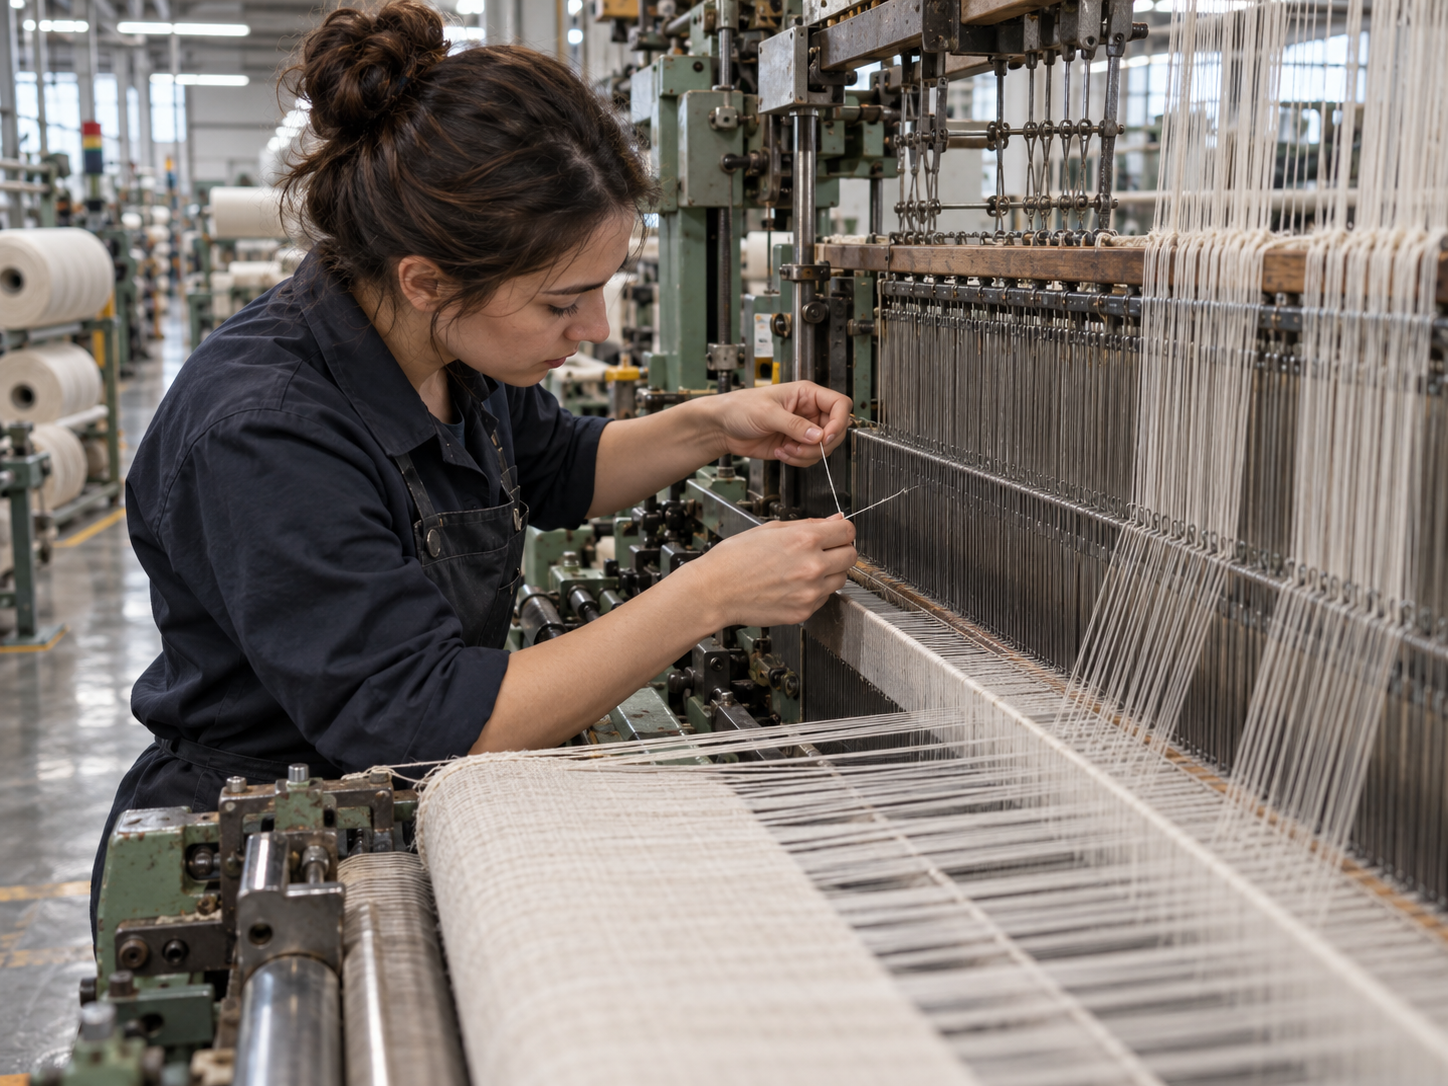
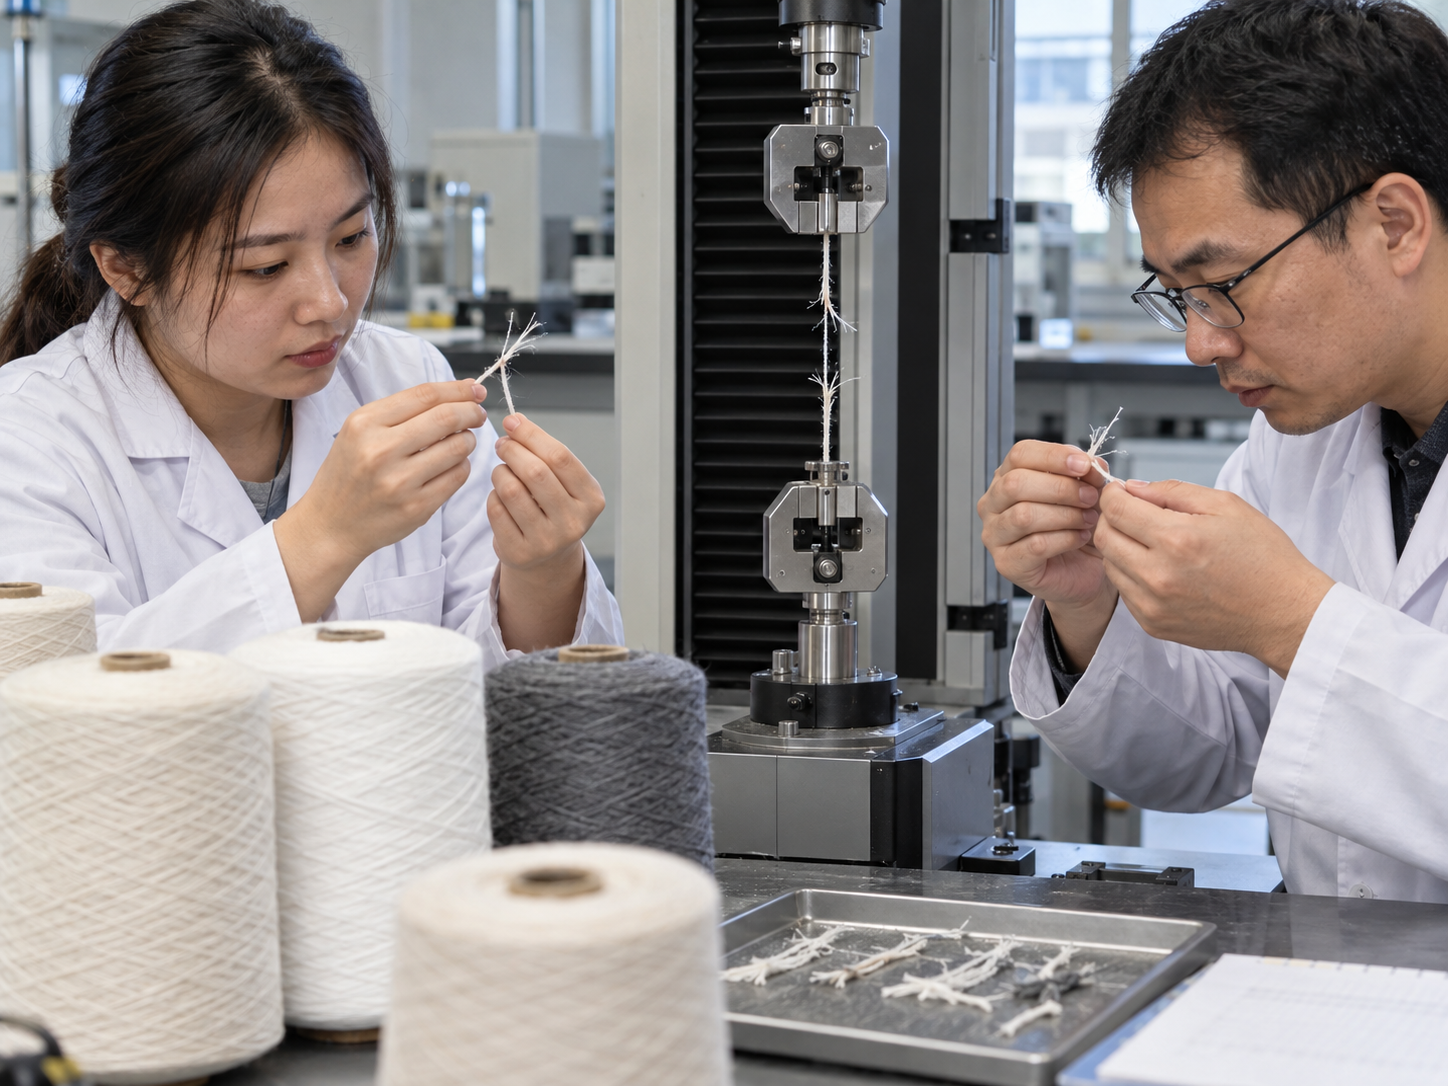
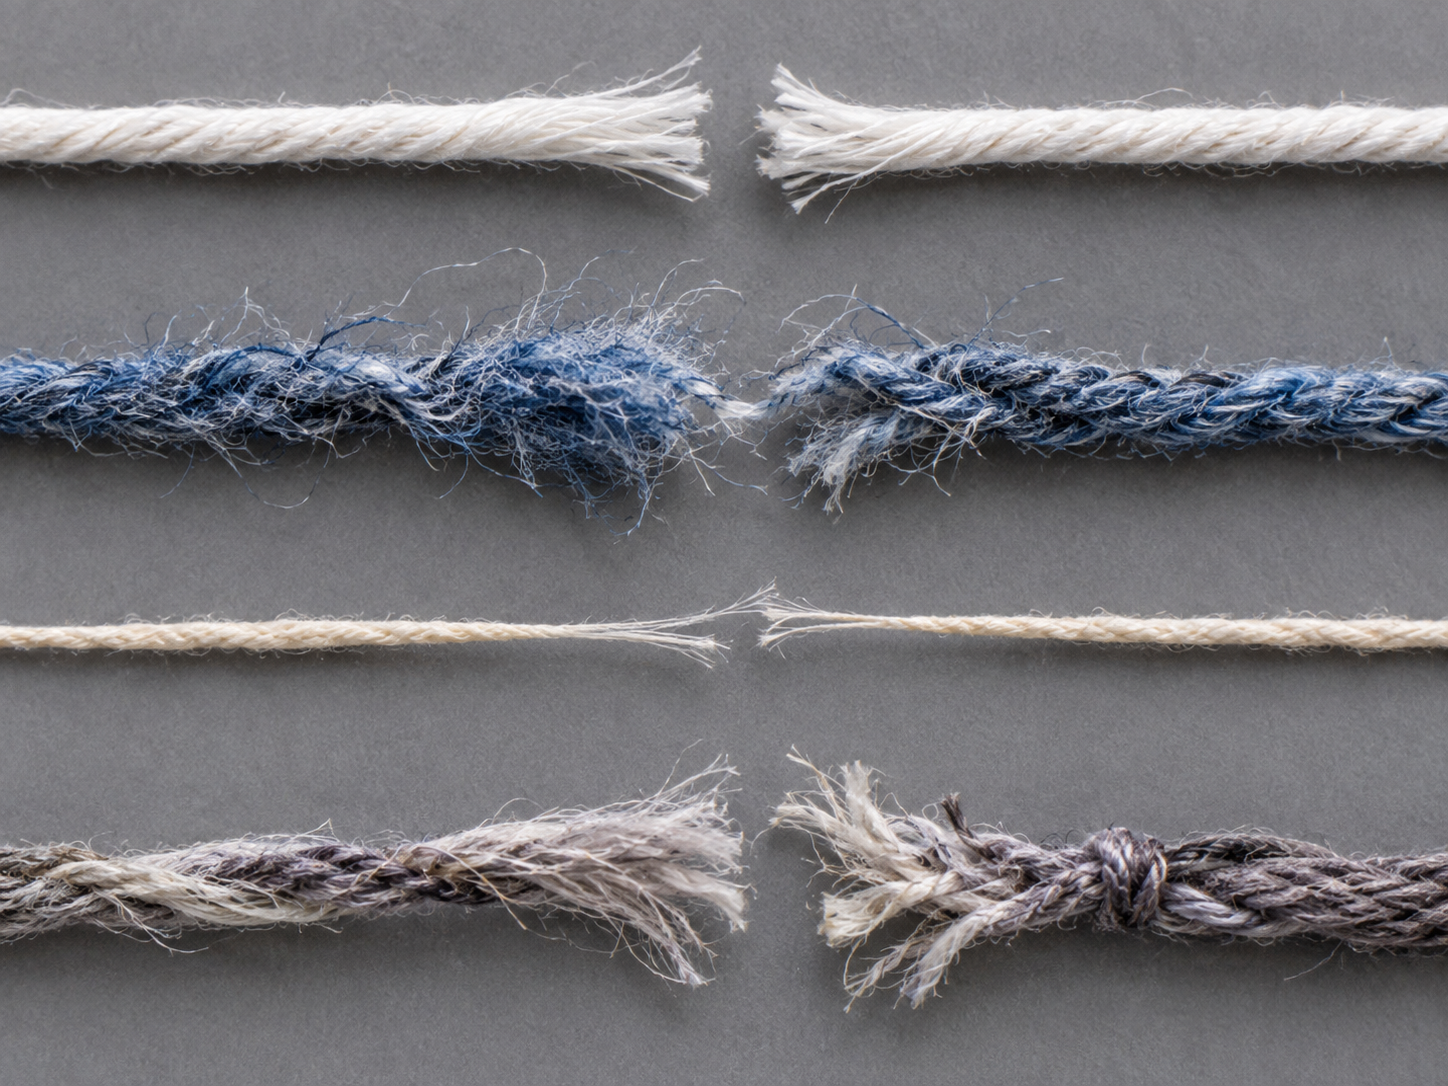
In textile manufacturing, a break usually means the unintended rupture of a yarn, filament, end, pick or thread while it is being formed, prepared, processed or converted into fabric. The exact meaning depends on the stage of production. Spinners commonly speak of end breaks during yarn formation; weavers distinguish warp-end and weft breaks; knitters encounter yarn breaks that may create holes, dropped stitches or machine stoppages. A break is therefore not one single defect but a process event with consequences for productivity, fabric quality and operating stability.
Breakage matters because textile processes operate under controlled tension at high speed. A yarn that is sufficiently strong under a laboratory tensile test may still fail in production if it contains a local weak place, is abraded by machine parts, experiences a sudden tension peak, is too dry, has a poor splice or is poorly matched to the process. Understanding breaks requires both material knowledge and process diagnosis: fibre properties, yarn structure, evenness, twist, elongation, package quality, machine condition, tension control and environmental conditions can all contribute. The practical goal is not to chase an arbitrary zero-break target, but to identify abnormal break patterns and remove the causes that reduce quality or efficiency.
What a Break Means in Textile Production
Textile terminology uses the word break in several related ways. A yarn break is the physical rupture of a yarn. An end break usually refers to one running yarn end that fails during spinning, winding, warping, sizing or weaving. In weaving, a warp break is the failure of a lengthwise yarn, while a weft break concerns the crosswise yarn. A broken pick may appear in fabric when part of a weft insertion is missing. In knitting, yarn breakage during loop formation can lead to holes, cracks, dropped stitches or machine stoppages.
These events should be distinguished from laboratory terms such as breaking force, which is the measured force at which a specimen ruptures, and elongation at break, which describes how much the specimen extends before failure. A production break is an event in a dynamic system; breaking force and elongation are measured material properties. The distinction is important because process breakage is influenced not only by average yarn strength, but also by local weak places, friction, tension fluctuations, machine geometry, package defects and handling history.
How Yarn Rupture Occurs
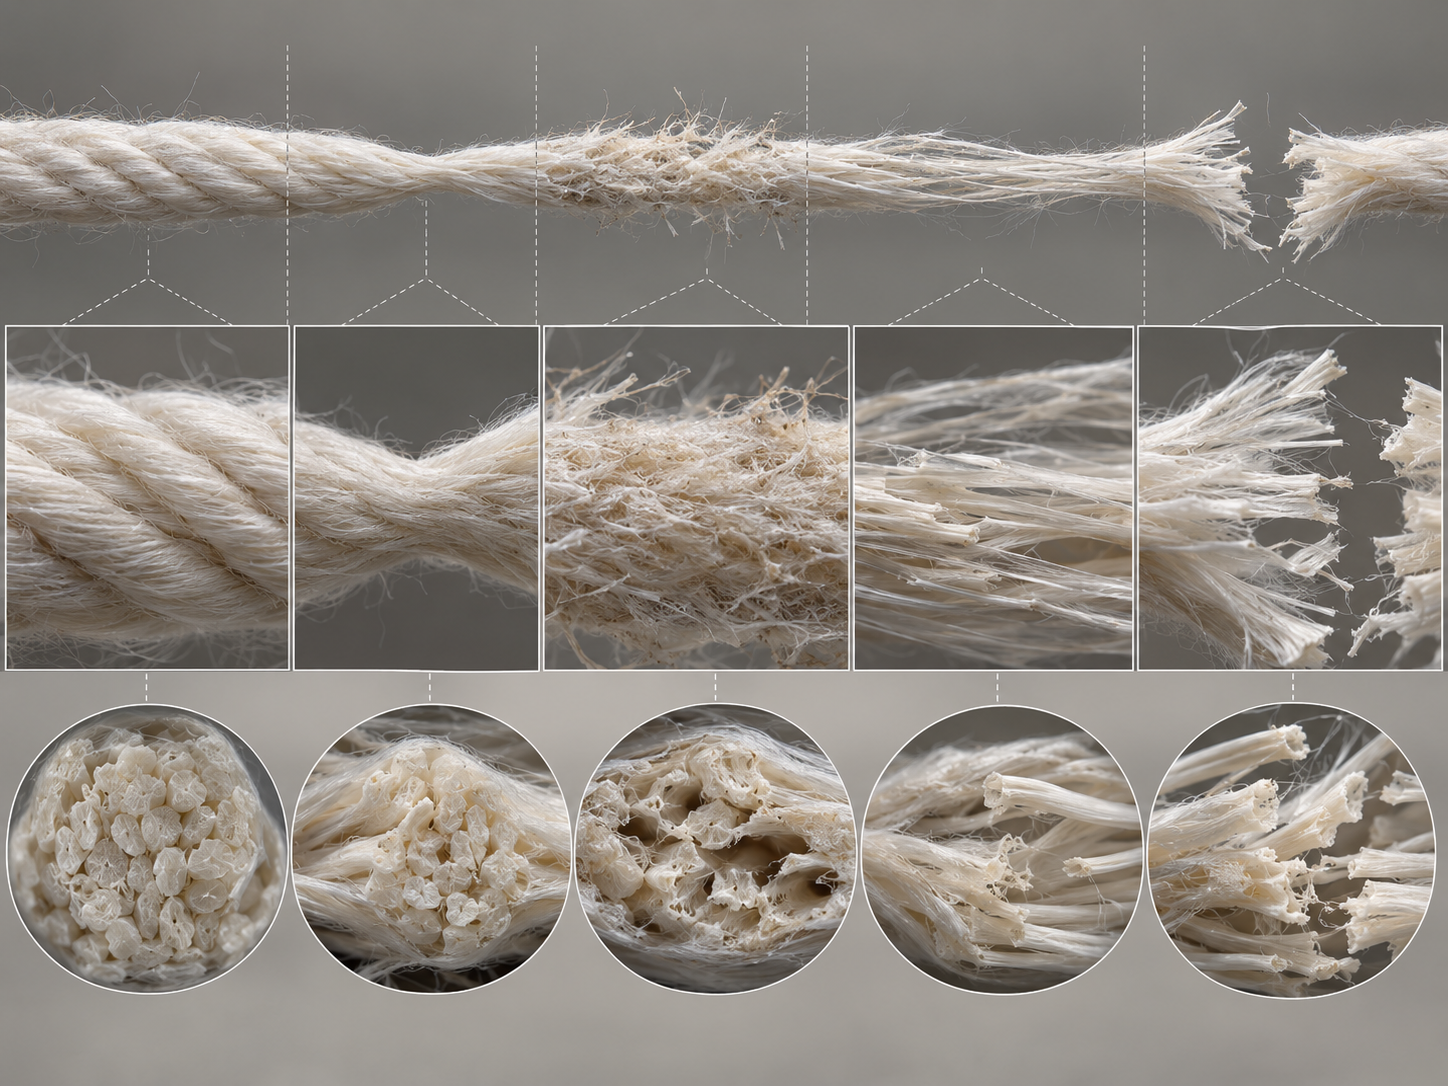
A running yarn fails when the stress imposed on a critical section exceeds the local resistance of that section. The critical point is often not representative of the average yarn. A thin place, damaged fibre bundle, poorly consolidated splice, knot, abrasion zone or irregular twist region can concentrate stress and become the first location to rupture. This is why two yarns with similar average tensile results can behave differently on a machine if one has more severe local faults.
Failure may be predominantly tensile, abrasive or mixed. Pure tensile rupture occurs when tension rises beyond the yarn's load-bearing capacity. Abrasion progressively removes or damages fibres until the remaining structure cannot carry the load. Repeated bending over guides can add fatigue. Sudden acceleration, ballooning, package unwinding disturbances or a yarn catching on a rough surface can create short-lived tension peaks that are much higher than the normal running tension. In spun yarns, fibre cohesion and twist help transfer load among fibres; in continuous-filament yarns, filament damage, broken filaments and surface defects can become critical. The mechanism must therefore be diagnosed from the break location and operating conditions rather than from tensile strength alone.
Breaks During Spinning
During spinning, end breaks interrupt yarn formation and require piecing or automatic restoration. Their causes can originate in the fibre assembly, the drafting zone, twist insertion, traveller or rotor conditions, package build, contamination, humidity or machine settings. Irregular drafting can create thin places that have insufficient fibres in the yarn cross-section. In ring spinning, an imbalance among delivery speed, twist, balloon tension and traveller behaviour can raise stress on the newly formed yarn. Excessive friction, worn parts or poor alignment can add further load.
Fibre length, fineness, strength, cleanliness and cohesion influence how reliably fibres form a continuous strand. Short fibres or poorly controlled drafting can reduce local structural integrity. Uneven sliver or roving can carry variation forward into the yarn. Break analysis should therefore connect the spinning frame to upstream preparation such as carding, drawing and roving rather than treating the frame as an isolated machine. A useful investigation compares break frequency by position, count, lot, spindle or machine section and then examines whether failures cluster around the same mechanical location, raw-material batch or yarn irregularity pattern. Persistent clustering usually indicates a specific cause rather than normal random variation.
Winding, Warping and Sizing Breaks
Yarn preparation stages expose yarn to repeated acceleration, guides, tension devices and package transfer. Winding can remove objectionable faults and create better packages, but it can also introduce problems if clearing settings are inappropriate, splices are weak or package density and traverse are poorly controlled. A splice that looks acceptable may still fail later if its strength, structure or diameter differs too much from the parent yarn.
Warping multiplies the importance of individual-end reliability because many ends run simultaneously. One weak or damaged end can stop the process or create downstream problems in sizing and weaving. Sizing is used mainly to improve warp abrasion resistance and cohesion for weaving, but poor size preparation, uneven add-on, excessive brittleness, inadequate drying or unsuitable moisture can reduce performance instead of improving it. Tension should be controlled through the full path: creel, guides, stop motions, lease rods, sizing elements, drying and beam build. When breakage rises after a preparation change, the investigation should compare yarn properties before and after that stage and inspect the exact break appearance for abrasion, brittle fracture, weak splices or tension-related failure.
Warp and Weft Breaks in Weaving
Weaving places severe demands on yarn because warp ends are repeatedly tensioned, bent and abraded while the shed opens and closes. The loom may also subject yarn to contact with heddles, reeds, drop wires and other surfaces. Research by James Lappage on weavable singles yarns identified failed splices, abrasion failure and thin places as important causes of weaving end breaks. The same study found that thin-place break incidence increased as yarn irregularity increased and as linear density became finer.
Warp break diagnosis should therefore combine loom inspection with yarn-quality information. Rough heddle eyes, damaged reeds, poor alignment, excessive warp tension or uneven beam build can create machine-specific break patterns. Yarn-side causes include low local strength, irregularity, poor sizing, weak joints and abrasion sensitivity. Weft failures differ with insertion technology, but excessive insertion tension, poor package unwinding, damaged guides or unsuitable joints can all contribute. A broken pick or partial missing pick is not merely a productivity event; if not detected and repaired correctly it can become a visible fabric defect. Modern stop motions help prevent continued weaving after a failure, but they do not remove the root cause.
Breaks in Knitting
Knitting forms fabric by repeatedly drawing yarn into loops, so the yarn must tolerate rapid changes in tension, bending and contact with needles and guides. A break during loop formation can produce holes, cracks, dropped stitches or a machine stop. Educational material from INFLIBNET identifies high yarn irregularity, weak places, knots or slubs and excessively dry yarn among possible yarn-related causes of holes or cracks associated with breakage.
Knitting breakage can also arise from machine conditions. Damaged needles, rough yarn paths, excessive feeder tension, incorrect take-down relationships, poor lubrication or contamination may create local stress. Yarn properties must match the gauge and fabric structure: a yarn that performs well on one machine may be less suitable for a finer gauge or a tighter construction. Knitting faults should be examined by position and repeat pattern. If defects recur in the same feeder or needle track, the machine path deserves priority. If they move with the yarn package or lot, material quality becomes more likely. Because small holes can arise from different mechanisms, diagnosis should rely on the process history and physical evidence rather than on appearance alone.
Material and Yarn Properties That Influence Breakage
Several yarn properties influence break resistance, but no single value predicts performance in every process. Breaking force indicates the load required to rupture a specimen. Tenacity relates breaking force to linear density, allowing more meaningful comparison among yarns of different sizes. Elongation at break indicates how much extension the yarn can tolerate before rupture. A yarn with reasonable strength but very limited extensibility may respond poorly to short tension peaks, while a more extensible yarn can sometimes absorb transient strain.
Evenness is especially important because the weakest local section governs many process failures. Thin places may contain fewer load-bearing fibres and can become preferred break points. Twist affects cohesion in spun yarns: insufficient twist may reduce fibre binding, while excessive twist can change extensibility, handling and downstream performance. Fibre length, fineness, strength and frictional behaviour influence yarn structure. Moisture and conditioning also matter because many fibres respond to relative humidity. For continuous-filament yarns, filament damage, entanglement quality, finish and friction become significant. Quality control should therefore evaluate a property profile rather than treating average breaking strength as the sole acceptance criterion.
Testing Breaking Force and Elongation
Standardized tensile testing provides a controlled basis for comparing yarn performance. ISO 2062:2009 specifies methods for determining the breaking force and elongation at break of yarns from packages using constant-rate-of-extension equipment. It describes several specimen preparation and conditioning routes, including conditioned packages, relaxed test skeins and wet testing. As of 2026, ISO lists ISO 2062:2009 as the published standard while a committee draft for a new edition is under development.
ASTM D2256/D2256M covers single-strand tensile properties of many monofilament, multifilament and spun yarns and includes measurement of breaking force and elongation, with calculations such as tenacity, modulus and breaking toughness. These laboratory methods are valuable because they control gauge length, specimen handling and rate of extension. However, a production machine adds abrasion, bending, dynamic tension and repeated contact that a simple tensile test does not fully reproduce. For break investigations, tensile data should be interpreted together with yarn evenness, fault data, splice quality, abrasion evidence, moisture condition and machine observations. The objective is to link measured material properties with the actual failure mechanism.
A Practical Troubleshooting Method
Effective troubleshooting starts by defining the break precisely: where it occurred, which yarn or end failed, what the machine was doing, and whether the failure repeats. Operators should preserve representative broken ends when possible and note the position, package, lot, machine side, speed, tension setting and visible fracture character. A clean rupture, fuzzy abrasion break, weak splice failure and snagged end provide different clues.
- Localize the pattern: determine whether breaks cluster by machine position, package, spindle, beam, feeder, yarn lot or time period.
- Inspect the yarn path: look for rough guides, damaged surfaces, alignment problems, excessive wrap angles and contamination.
- Check tension and dynamics: compare normal running tension with start-up, acceleration and package-unwinding behaviour.
- Review yarn quality: examine strength, elongation, evenness, faults, joints and moisture condition.
- Change one factor at a time: controlled trials make cause-and-effect visible and prevent multiple simultaneous adjustments from hiding the real cause.
The most useful result is a verified mechanism, not merely a lower break count after several uncontrolled adjustments.
Production, Quality and Sustainability Impacts
Breaks reduce productivity because machines slow or stop, operators or automatic systems must restore the yarn path, and subsequent quality checks may be required. Frequent breaks can also increase waste through discarded yarn, faulty fabric, rework and downgraded production. In weaving, repeated warp breaks may cause repair marks or variation if handling is inconsistent. In knitting, a missed break can become a hole or dropped-stitch defect. In spinning and winding, repeated piecing can affect package quality and downstream consistency.
There is also a sustainability dimension. Preventing avoidable breakage can reduce wasted fibre, yarn, fabric, energy and machine time. However, process control should not simply increase chemical use, size add-on or yarn mass to suppress breaks. The better approach is to match raw material, yarn design, preparation and machine settings to the required product. Predictive maintenance, online tension monitoring, yarn clearing, fault mapping and better data capture can make troubleshooting more selective. A lower and more stable break rate achieved through control of weak places, friction and tension is generally more valuable than a temporary reduction obtained by over-processing the yarn.
Why Break Control Matters to Textile Quality and Efficiency
A textile break is a small event with system-wide consequences. Whether it occurs during spinning, winding, warping, weaving or knitting, it represents a moment when the local strength and extensibility of the yarn are no longer sufficient for the mechanical demands imposed on it. The important word is local: average strength can look acceptable while a thin place, damaged region, weak splice or abraded section still becomes the point of failure. That is why break control depends on both laboratory testing and direct process evidence.
The most reliable control strategy combines yarn quality, machine condition and process dynamics. Breaking force, tenacity, elongation, evenness, fibre properties and joint quality describe the material side. Tension peaks, guide condition, alignment, abrasion, humidity, package unwinding and machine settings describe the process side. When these are investigated together, recurring break patterns can usually be narrowed to a small number of plausible mechanisms instead of being treated as random stoppages.
Future textile production will increasingly use online sensing, automated fault classification and data-driven maintenance to identify abnormal break patterns earlier. Yet the underlying engineering principle remains unchanged: prevent weak locations from meeting excessive stress. Mills that treat breaks as diagnostic information rather than isolated interruptions can improve productivity, reduce defects and waste, and make process settings more robust across changing yarn lots, machine speeds and fabric constructions.